





Welding gas mixtures are shielding gases used to protect the weld pool and arc from atmospheric contamination during gas-shielded welding. The composition of the shielding gas can affect arc stability, metal transfer, spatter, penetration, weld bead shape, and overall welding productivity.
Common welding gases include argon, helium, carbon dioxide, oxygen, and specialized mixtures containing hydrogen or nitrogen. The appropriate gas depends on the welding process, base metal, material thickness, transfer mode, filler metal, and required weld characteristics.
This guide explains the most common welding gas mixtures, including Ar/CO2, Ar/O2, Ar/He, and three-component mixtures, and explains how to select a suitable shielding gas for carbon steel, stainless steel, aluminum, copper, and other applications.
What Is a Welding Gas Mixture?
A welding gas mixture is a controlled combination of two or more gases used as a shielding gas during welding. The gas flows around the arc and weld pool to reduce exposure to atmospheric gases such as oxygen and nitrogen.
Depending on the application, a welding gas may be:
- A pure gas, such as 100% argon or 100% carbon dioxide
- A binary mixture, such as argon/CO2 or argon/helium
- A ternary mixture, such as argon/CO2/O2 or argon/helium/CO2
- A specialized mixture containing hydrogen, nitrogen, or other components
The term shielding gas is commonly used because the gas creates a protective atmosphere around the welding arc and molten metal. Different gas compositions produce different welding characteristics, so gas selection should be matched to the welding procedure rather than based on the gas name alone.
Common Welding Gas Mixtures
| Welding Gas | Typical Composition | Common Applications | Key Characteristics |
|---|---|---|---|
| Argon | 100% Ar | TIG; MIG of aluminum and other non-ferrous metals | Stable arc and good control |
| C25 / 75/25 | 75% Ar + 25% CO2 | MIG/MAG welding of carbon and low-alloy steel | Common balance of penetration, arc characteristics, and productivity |
| Ar/CO2 | Argon with a controlled percentage of CO2 | MAG welding of carbon and low-alloy steel | Gas composition influences penetration, transfer mode, and spatter |
| Ar/O2 | Argon with a small percentage of O2 | MAG welding of steel | Can improve arc stability and wetting |
| Ar/He | Argon + helium | Aluminum, copper, and other non-ferrous metals | Higher heat input than pure argon |
| Ar/He/CO2 | Argon + helium + CO2 | Selected stainless steel and steel applications | Can provide a broader heat distribution and useful penetration characteristics |
These are representative gas families rather than universal formulas. Commercial gas suppliers may offer different compositions for specific welding processes and materials. The required gas should therefore be selected according to the welding procedure, filler-metal recommendations and applicable standards.

Welding Gas Selection by Welding Process
MIG Welding Gas
MIG stands for Metal Inert Gas. In MIG welding, inert shielding gases such as argon and helium are commonly used, particularly for aluminum and other non-ferrous metals.
Common choices include:
- 100% argon
- Argon/helium mixtures
- Specialized inert gas mixtures for specific applications
Pure argon is widely used for aluminum MIG welding because it provides a stable arc and is suitable for many aluminum welding applications. Argon/helium mixtures may be selected when additional heat input is desirable.
MAG Welding Gas
MAG stands for Metal Active Gas. Active shielding gases are primarily used for welding steels. Typical gases include carbon dioxide and argon-based mixtures containing carbon dioxide and/or oxygen.
Examples include:
- CO2
- Ar + CO2
- Ar + O2
- Ar + CO2 + O2
The gas composition has a substantial effect on arc stability, metal transfer, spatter, penetration and weld-pool behavior. Therefore, the same welding machine and wire may require different shielding gas selections for different applications.
TIG Welding Gas
TIG welding normally uses an inert or reducing shielding atmosphere. Argon is one of the most widely used TIG shielding gases, while helium and selected argon/helium or argon/hydrogen mixtures may be used for specialized applications.
For TIG welding, gas selection can affect arc characteristics, heat input and welding speed. Hydrogen-containing mixtures require particular attention to material compatibility and the applicable welding procedure.
What Is 75/25 Welding Gas?
75/25 welding gas normally refers to a shielding gas containing approximately 75% argon and 25% carbon dioxide. It is also commonly called C25 gas.
C25 is widely used for MIG/MAG welding of carbon and low-alloy steels. A 75% argon / 25% CO2 mixture is one example of the Ar/CO2 family used for steel welding. However, it should not be considered the universal best gas for every MIG application.
The appropriate Ar/CO2 ratio depends on factors such as:
- Base metal
- Material thickness
- Filler wire
- Welding current and voltage
- Metal transfer mode
- Welding position
- Required penetration and weld appearance
For this reason, a welding procedure specification (WPS), filler-metal manufacturer’s recommendation, or equipment manufacturer’s guidance should be followed when selecting the final gas composition.
Argon and CO2 Welding Gas Mixtures
Argon/CO2 mixtures are among the most widely used shielding gases for MAG welding of carbon and low-alloy steels.
Increasing or decreasing the CO2 concentration changes the behavior of the welding arc and weld pool. In general, higher CO2 content can increase penetration but may also increase spatter depending on the welding conditions. Higher argon content can provide different arc and transfer characteristics.
Common commercial mixtures may include compositions such as:
- 75% Ar / 25% CO2
- 80% Ar / 20% CO2
- 82% Ar / 18% CO2
- 90% Ar / 10% CO2
- Higher-argon mixtures for specific transfer modes and applications
The exact mixture should be selected according to the welding process and procedure rather than simply choosing the highest or lowest CO2 concentration.
Argon and Oxygen Welding Gas Mixtures
Argon/oxygen mixtures are active shielding gases used primarily for MAG welding of steel. Small additions of oxygen to argon can influence arc stability, droplet transfer and wetting.
Typical industrial shielding gases may contain approximately 1–5% oxygen in argon, depending on the welding application. TWI identifies argon with approximately 2–5% oxygen as one of the shielding-gas options used for steels.
Because oxygen is an active component, the appropriate concentration depends on the material, filler metal and welding procedure. Oxygen-containing mixtures should not be treated as interchangeable with pure argon.
Argon and Helium Welding Gas Mixtures
Argon/helium mixtures are commonly used for non-ferrous metals such as aluminum and copper and in selected other applications.
Helium has different thermal characteristics from argon and can provide higher heat input. This can be useful when welding materials or sections where additional heat is required.
Argon/helium mixtures may therefore be considered for:
- Aluminum
- Copper and copper alloys
- Nickel alloys
- Thicker non-ferrous sections
- Applications requiring increased heat input
The helium concentration can vary substantially between commercial mixtures. Specialized welding procedures may use mixtures with different proportions of argon and helium to achieve the required arc and heat-transfer characteristics.
Argon, Helium and CO2 Mixtures
Three-component shielding gases containing argon, helium and carbon dioxide are used for selected steel and stainless-steel welding applications.
Helium can increase thermal conductivity and heat input, while argon contributes to arc characteristics and CO2 provides an active component for MAG welding. The combined effect can produce welding characteristics that are different from a simple Ar/CO2 mixture.
These mixtures are sometimes referred to as tri-mix gases. However, “tri-mix” does not represent one universal gas composition. Different suppliers may use different ratios for different applications.
For this reason, when purchasing a tri-mix welding gas, always specify the actual gas composition rather than ordering only by the term “tri-mix.”
Welding Gas Mixture for Carbon Steel
Carbon steel is commonly welded using CO2 or argon-based active gas mixtures.
Typical choices include:
- 100% CO2
- Ar/CO2 mixtures
- Ar/O2 mixtures
- Ar/CO2/O2 mixtures for selected applications
Ar/CO2 mixtures are particularly common because they can provide a useful balance between penetration, arc behavior and spatter characteristics.
For production welding, the gas should be selected together with the wire diameter, filler-metal classification, current, voltage, travel speed and transfer mode.
Welding Gas Mixture for Stainless Steel
Stainless steel requires careful shielding-gas selection because the gas can affect arc behavior, weld-pool fluidity, penetration, bead appearance and the resulting weld properties.
Depending on the process and stainless-steel grade, applications may use:
- Argon-based mixtures
- Argon/oxygen mixtures with controlled oxygen content
- Argon/CO2 mixtures with controlled CO2 content
- Argon/helium/CO2 mixtures
- Specialized shielding gases for particular welding procedures
For example, helium-containing ternary mixtures are used in some stainless-steel applications where higher heat input, weld-pool fluidity or a different bead profile is required.
The correct gas should always be matched to the stainless-steel grade, welding process, filler metal and qualified welding procedure.
Welding Gas Mixture for Aluminum
100% argon is a common shielding gas for aluminum welding, including many TIG and MIG applications.
Argon/helium mixtures may be selected when additional heat input is desirable, particularly for thicker aluminum sections or applications where increased welding productivity is required.
When selecting gas for aluminum, consider:
- Aluminum alloy
- Material thickness
- MIG or TIG process
- AC or DC welding requirements where applicable
- Wire or filler-metal selection
- Required travel speed
- Joint configuration
Gas selection should be made together with the complete welding procedure rather than independently.
Welding Gas Mixture for Copper
Copper and copper alloys have high thermal conductivity, which can make heat input an important consideration during welding.
Argon is commonly used for copper and copper-alloy welding, while argon/helium mixtures may be considered where additional heat input is beneficial.
The appropriate mixture depends on the copper alloy, thickness, welding process, joint design and required welding performance.
How Does Welding Gas Composition Affect Welding?
The composition of a shielding gas can influence several important welding characteristics.
1. Arc Stability
The gas composition affects the electrical characteristics of the arc and therefore influences arc stability and metal transfer.
2. Penetration
Different gas mixtures can produce different penetration profiles. For example, increasing the active component in an Ar/CO2 mixture can affect penetration and arc behavior.
3. Spatter
Shielding gas composition can affect droplet transfer and the amount of spatter produced during welding. Argon-based mixtures are often selected when controlled transfer and reduced spatter are important.
4. Weld Bead Shape
The shielding gas can influence weld-pool fluidity, wetting and bead profile. This becomes particularly important in automated and high-productivity welding.
5. Heat Input
Helium-containing mixtures can provide increased heat input compared with pure argon in suitable applications. This can be useful for some thick-section or high-productivity welding operations.
Because these effects interact with welding current, voltage, travel speed, wire feed speed and transfer mode, gas selection should always be considered as part of the complete welding procedure.
How to Choose the Right Welding Gas Mixture
There is no single welding gas mixture that is suitable for every welding application. A practical gas-selection process should consider the following factors.
1. Identify the Welding Process
First determine whether the application uses MIG, MAG, TIG, plasma or another gas-shielded process.
2. Identify the Base Metal
Determine whether the material is carbon steel, stainless steel, aluminum, copper, nickel alloy or another metal.
3. Check Material Thickness
Thicker sections may require different heat-input characteristics from thin materials. Gas mixtures containing helium may be considered in applications where additional heat input is required.
4. Check the Metal Transfer Mode
MIG/MAG transfer modes include short-circuiting, globular, spray and pulsed transfer. The appropriate shielding gas can vary with the transfer mode.
5. Check the Filler Metal
The filler wire or electrode classification should be considered when selecting the shielding gas. The filler-metal manufacturer may specify recommended shielding gases.
6. Consider the Required Weld Characteristics
Determine whether the priority is penetration, low spatter, bead appearance, productivity, arc stability, welding speed or another characteristic.
7. Follow the Welding Procedure
For production welding, the shielding gas should be consistent with the qualified welding procedure, applicable standards and customer requirements.
Pure Gas vs. Welding Gas Mixture
| Gas Type | Typical Advantage | Typical Applications |
|---|---|---|
| 100% Argon | Stable inert shielding and good arc control | TIG; MIG of aluminum and other non-ferrous metals |
| 100% CO2 | Active shielding and useful penetration characteristics | Selected MAG applications |
| Ar/CO2 | Balance of arc behavior and penetration characteristics | Carbon and low-alloy steel |
| Ar/O2 | Arc stabilization and wetting characteristics | Selected steel MAG applications |
| Ar/He | Higher heat input in suitable applications | Aluminum, copper, and other non-ferrous metals |
| Multi-component Mixtures | Tailored welding characteristics | Specialized steel and stainless-steel applications |
Welding Gas Mixture Cylinders
Welding gas mixtures are commonly supplied in high-pressure gas cylinders for welding shops, fabrication facilities and industrial gas distributors.
For cylinder supply, important considerations include:
- Gas composition and purity
- Cylinder working pressure
- Water capacity
- Applicable cylinder standard
- Valve specification
- Filling and testing requirements
- Gas compatibility
- Transport and storage requirements
When purchasing a cylinder for a welding gas mixture, the cylinder itself should be compatible with the gas service and the applicable local regulations and standards.
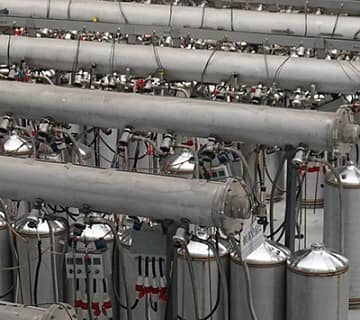
For larger welding operations, gas may also be supplied through multiple-cylinder manifolds, cylinder bundles, bulk systems or other industrial gas supply arrangements.
Welding Gas Supply for Industrial Applications
Small welding shops may use individual cylinders, while larger fabrication facilities can require a centralized gas supply system.
A typical industrial welding gas supply system may include:
- Welding gas cylinders
- Cylinder bundles
- Manifolds
- Pressure regulators
- Gas distribution pipelines
- Valves and safety devices
- Point-of-use gas outlets
- Gas monitoring and control equipment
The appropriate supply method depends on gas consumption, number of welding stations, required pressure, plant layout and operating conditions.
For larger industrial applications, see our guide to industrial gas supply systems.
Welding Gas Mixture Storage and Handling
Welding gases must be stored and handled according to the applicable safety requirements for compressed gases.
- Secure cylinders to prevent tipping or falling.
- Keep cylinders away from excessive heat and physical damage.
- Use the correct regulator and connection for the gas service.
- Keep valves and connections clean and free from contamination.
- Check cylinders, valves, hoses and regulators before use.
- Provide adequate ventilation in areas where compressed gases are stored or used.
- Do not use a gas cylinder for a service for which it is not approved.
Many welding shielding gases are colorless and odorless. Inadequate ventilation can allow inert or other gases to accumulate and reduce oxygen concentration, creating an asphyxiation hazard. Appropriate ventilation, gas-handling procedures and workplace safety controls are therefore essential.
Conclusion
Welding gas mixtures play an important role in MIG, MAG and TIG welding. Argon, carbon dioxide, helium and oxygen are combined in different proportions to produce shielding gases with different arc, penetration, transfer and weld-pool characteristics.
For carbon steel, Ar/CO2 and other active gas mixtures are widely used. For aluminum and other non-ferrous metals, argon and argon/helium mixtures are common. Stainless steel and specialized applications may require more carefully controlled multi-component shielding gases.
The best approach is not to select a welding gas based on a single universal ratio. Instead, match the gas composition to the welding process, base metal, thickness, filler metal, transfer mode and qualified welding procedure.
DSW supplies gas cylinders and equipment for industrial gas applications and can support different gas storage, cylinder and supply requirements. For welding gas cylinder requirements, see our gas cylinder guide or contact DSW for your application requirements.
TECHNICAL QUESTIONS
About Welding Gas Mixtures
The appropriate MIG shielding gas depends on the base metal and welding application. Argon is widely used for aluminum and other non-ferrous metals, while argon-based active mixtures are commonly used for steel MAG applications.
75/25 welding gas normally means a mixture containing approximately 75% argon and 25% carbon dioxide. It is also commonly known as C25 and is widely used for carbon-steel MIG/MAG welding.
In common industrial usage, C25 and 75/25 refer to approximately the same argon/CO2 composition: 75% argon and 25% carbon dioxide. Always confirm the actual composition on the gas specification or cylinder label.
100% argon is a common choice for aluminum MIG welding. Argon/helium mixtures may also be used for selected applications where increased heat input is desirable.
MAG welding of steels commonly uses carbon dioxide or argon-based mixtures containing carbon dioxide and/or oxygen. The appropriate composition depends on the welding procedure and application.
Tri-mix generally describes a shielding gas containing three components, such as argon, helium and carbon dioxide. There is no single universal tri-mix composition, so the actual gas percentages should always be specified.
No. Welding gas selection depends on the welding process, base metal, thickness, filler metal, transfer mode and required weld characteristics. A gas suitable for carbon steel may not be suitable for aluminum or stainless steel.
Specify the complete gas composition and required purity rather than relying only on a commercial name such as C25 or tri-mix. For production applications, also provide the welding process, material, filler metal and applicable welding procedure.

No comment